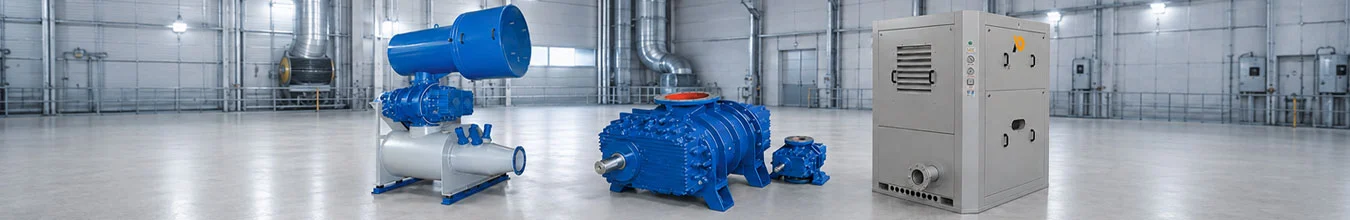
In metal-finishing systems, roots blowers for surface treatment may supply air for selected bath-agitation duties when process conditions permit. Common methods include electroplating, anodizing, chemical conversion, cleaning, pickling, rinsing, painting and thermal coating.
Roots blowers are not directly involved in every surface treatment method. Their principal role is to provide continuous, oil-free, low-pressure air for applications such as process-bath agitation, rinse-water circulation and certain air-knife blow-off systems.
Electroplating and anodizing represent particularly relevant applications. In these processes, air can be introduced through perforated sparger pipes installed near the bottom of a tank. The rising bubbles create bulk liquid movement, reduce localized concentration differences and help maintain more uniform conditions around the treated components.
Because a roots blower is a positive-displacement machine, it can maintain a relatively stable airflow against the backpressure created by liquid depth, pipework and sparger openings. This makes the technology suitable for surface treatment lines requiring continuous air delivery over extended production periods.
Air Agitation in Process Tanks
During electroplating, metal ions must move through the electrolyte toward the component surface. A relatively stagnant boundary layer can form next to the workpiece, limiting mass transfer and contributing to concentration polarization.
Correctly applied agitation renews the solution near the component surface and can support:
- More uniform ion distribution
- Improved mass transfer
- Reduced concentration gradients
- More consistent coating thickness
- Removal of gas bubbles from component surfaces
- Improved temperature uniformity
- Increased allowable current density in suitable processes
- More consistent surface appearance
In anodizing tanks, agitation can help distribute heat and maintain relatively uniform electrolyte conditions. It can also remove gas bubbles that would otherwise remain on component surfaces and interfere with oxide-film formation.
Air agitation is commonly produced by placing perforated sparger pipes below or beside the working area. Air from the blower passes through the openings, forms bubbles and rises through the solution.
The required blower pressure must overcome the hydrostatic pressure of the solution and all additional system losses:
Required Blower Discharge Pressure
- prequired = required blower discharge pressure
- ρ = density of the process solution
- g = gravitational acceleration
- h = liquid depth above the sparger
- Δppipe = pressure loss through the air pipeline
- Δpvalve = pressure loss through valves and fittings
- Δpsparger = pressure loss through the sparger openings
For water at standard conditions, hydrostatic pressure increases by approximately 98.1 mbar for every metre of depth. Surface treatment solutions may have a higher density, producing a correspondingly greater hydrostatic load.
The blower must be selected for the required airflow at the total calculated pressure—not only for the tank depth. Undersized pipes, restrictive valves and improperly drilled spargers can increase backpressure significantly.
Airflow requirements depend on:
- Tank dimensions
- Effective process area
- Bath chemistry
- Required agitation intensity
- Component geometry and loading density
- Sparger length and arrangement
- Number and diameter of sparger holes
- Solution viscosity and density
- Process temperature
Excessive airflow is not necessarily beneficial. It can cause splashing, foaming, increased chemical mist, sediment disturbance and unnecessary energy consumption. The agitation rate should be approved by the process-chemical supplier and confirmed through production trials.
Rinse and Cleaning Tank Applications
Air agitation can also improve the performance of rinse and cleaning tanks. Components leaving a plating or chemical-treatment bath carry a thin film of process solution known as drag-out. This liquid must be removed before the component proceeds to the next stage.
Introducing air through bottom-mounted spargers creates liquid movement around the component and can reduce stagnant regions in the rinse tank. Effective mixing allows cleaner water to reach recesses, holes and irregular surfaces.
Benefits may include:
- Improved removal of drag-out solution
- More uniform rinse-water concentration
- Reduced short-circuiting within the tank
- Better contact with recessed component surfaces
- Potential reduction in freshwater consumption
- Lower chemical transfer to subsequent process stages
- Reduced wastewater loading
The rinse tank should still be designed according to the required water quality, component geometry and production rate. Air agitation cannot compensate for an inadequate rinse sequence, excessive drag-out or insufficient water replacement.
Air is not suitable for every cleaning solution. Certain formulations may foam excessively, oxidize or release additional mist when aerated. Mechanical circulation, pumped eductors or component movement may be preferable in these cases.
The blower intake should be positioned in a clean location away from acid fumes, solvent vapor and exhaust outlets. Drawing contaminated factory air into the blower and discharging it into a process bath can affect solution chemistry and product quality.
Solution Blow-Off and Air-Knife Systems
After a component leaves a process or rinse tank, liquid remaining on its surface can be removed with a directed air stream. An air knife produces a continuous sheet of high-velocity air that pushes liquid toward a collection area or back into the original tank.
Solution blow-off can:
- Reduce chemical drag-out
- Recover valuable process solution
- Lower contamination of rinse tanks
- Remove water before coating or drying
- Reduce the thermal load on drying ovens
- Minimize water spots on suitable surfaces
Roots blowers can supply an air-knife system where the required combination of pressure and airflow falls within the blower’s operating range. However, they are not the only available technology. Centrifugal and regenerative blowers are also commonly used.
The correct air source depends on air-knife width, outlet gap, required impact force, distance from the component, conveyor speed and part geometry. A roots blower should not be specified only because the application requires “blower air.”
Air knives are most effective when the air stream can reach the liquid directly. Complex components containing blind holes, cavities and overlapping surfaces may require multiple nozzles, component rotation or pulsed compressed air.
Solution blow-off must also be evaluated against surface chemistry. Some freshly treated metals can stain or oxidize if liquid is removed incorrectly or if the surface remains exposed before the next process stage.
Blower Package and Air Quality
A roots blower transports air without injecting lubricant into the process chamber. Under normal operating conditions, the air does not contact the oil used in the timing-gear and bearing compartments. This is an important advantage for plating and anodizing baths that can be damaged by oil contamination.
The correct technical term is “oil-free process air,” not “pure air.” Ambient air may still contain dust, humidity, aerosols or chemical vapor. Suitable inlet filtration and intake positioning are therefore necessary.
Glossary
Air knife: Slot nozzle that directs a high-velocity air sheet at a product surface.
Air-knife velocity: Air speed at the slot outlet used to remove liquid or debris from a surface.
Anodizing: Electrochemical growth of an oxide layer on a metal surface.
Electroplating: Electrochemical deposition of a metal coating onto a conductive workpiece.
Mist entrainment: Carryover of liquid droplets in air leaving a tank surface.
Pickling: Chemical cleaning step that removes oxide scale from a metal surface.
Sparger: Submerged pipe or nozzle that releases air into a process bath.
Tank ventilation rate: Airflow used to control vapors or mist above a process tank.