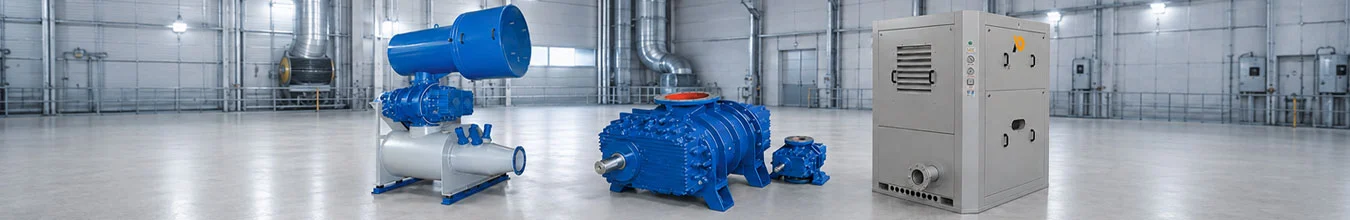
Biogas and biomethane blower systems support gas transfer, digester recirculation and selected treatment duties when the machine is matched to the gas composition, operating range, pressure requirements and package safety design. The application category includes several different services, so a blower selected for one gas stream should not automatically be specified for another.
For detailed technical articles, click here.
Roots blowers can be considered for process duties that fall within the selected machine’s verified flow, differential-pressure, temperature, speed and gas-compatibility limits. The correct review starts with the process duty and gas condition at the machine inlet—not with a generic air rating or the word “biogas” alone.
Define the Gas and Process Duty
Raw biogas composition varies with feedstock, digester operation and upstream treatment. Methane and carbon dioxide are its main components, while water vapour, hydrogen sulphide and, depending on the source, siloxanes and other trace compounds may also be present. These constituents affect corrosion risk, sealing, condensate formation, materials, gas density and the downstream user’s fuel-quality limits. Biomethane has been upgraded to a higher methane concentration, but its remaining contaminants, pressure and moisture still need to meet the receiving system’s specification.
For every blower duty, identify whether the machine handles raw biogas, treated biogas, biomethane, landfill gas, process air or a recycle/off-gas stream. State the gas analysis across minimum, normal and maximum conditions, along with suction pressure or vacuum, discharge pressure, temperature, actual or reference flow basis, operating hours and expected turndown. These details are necessary to assess performance and gas-wetted materials.
Gas Transfer to CHP Engines, Boilers, Flares and Treatment Systems
Biogas may move from a digester gas holder or landfill header through moisture removal, H₂S treatment, filtration and control equipment before reaching a combined heat and power (CHP) engine, boiler, flare or upgrading plant. A blower may provide transfer or a defined low-pressure boost where the complete pressure requirement—including filters, valves, piping and the final user’s inlet conditions—falls inside the approved operating envelope.
The duty should account for changes in gas production and consumption. CHP engines may change load or stop, boilers can follow heat demand, and flares may receive the excess flow when normal users are unavailable. Pressure control, storage capacity, standby philosophy and the required minimum and peak flow should be considered together. If the end user needs pressure beyond a low-pressure blower’s capability, a suitable compressor or staged arrangement may be required.
Landfill-Gas Collection Requires Controlled Extraction
Landfill-gas collection is a suction duty: a blower or other gas mover creates vacuum in wellfields and conveys the recovered gas to a flare, treatment system or beneficial-use equipment. The selected unit must match both the wellfield’s vacuum requirement and the pressure needed downstream. These two sides of the system should be reviewed as one duty.
Excessive extraction vacuum can draw air through covers, well seals or pipe connections, lowering methane quality and creating operating and safety concerns. Operators balance individual wells using gas composition, oxygen or nitrogen, temperature and pressure measurements. Landfill-gas output also changes over the project life, so staged units or variable-speed control may suit the expected operating range better than a single machine sized only for peak flow.
Anaerobic Digester Gas Recirculation and Mixing
In gas-recirculation systems, biogas is withdrawn from the digester headspace, routed through a gas-compatible blower and returned through submerged pipes or distribution devices. The rising bubbles can promote liquid or slurry circulation and help distribute feed, heat and microorganisms, depending on vessel geometry, solids content and the chosen mixing objective.
This is a closed process-gas loop, not an air-aeration duty. Its pressure requirement includes the liquid head at the injection point as well as pipe, valve and distributor resistance. The design must also address foam behaviour, condensate drainage, gas separation and operating limits of the digester. Gas recirculation should be specified separately from the blower that supplies fuel gas to CHP or upgrading equipment.
Biogas Upgrading: Apply the Article 224 Fit Boundary
Pressure-swing adsorption (PSA) and vacuum-pressure-swing adsorption (VPSA) plants use cyclic pressure conditions to separate methane from carbon dioxide and other constituents. Feed preparation, adsorption, depressurisation, pressure equalisation, purge and regeneration form one coordinated cycle. The blower or compressor requirement therefore depends on the upgrading process design, not simply on the fact that the skid uses PSA or VPSA.
A Roots machine may be considered for a defined low-pressure feed-transfer or pre-boost duty, selected recycle service, off-gas movement or a vacuum-regeneration step only when the process licensor’s cycle data and the machine’s performance limits support that role. These auxiliary duties must not be confused with the principal PSA pressurisation duty or the full VPSA vacuum duty. Where required pressure exceeds the blower envelope, the process needs a compressor; where regeneration requires deeper vacuum or greater capacity than the vacuum machine can provide, a suitable backing-pump arrangement may be necessary.
The final review should use the complete operating cycle, including gas composition, vessel volumes, starting and final pressures, evacuation time, purge flow, simultaneous vessel operation and recycle paths. A Roots blower is not a universal replacement for the compression or vacuum equipment selected by the upgrading-process designer.
Keep Biological H₂S Treatment Air Separate from Raw-Gas Service
Biological hydrogen-sulphide removal can use a dedicated air stream for an external biofilter or a carefully metered oxygen input in a treatment configuration designed for that purpose. The air blower in this application handles process air; it is not the raw-biogas blower. Airflow, oxygen concentration, H₂S load, treatment performance and interlocks should be set by the process design.
Uncontrolled air addition can dilute fuel gas and change its composition. Any oxygen dosing into a methane-containing stream therefore requires a defined operating method, monitoring and safety review. Specify the air-side equipment and the gas-side equipment as separate duties, including their respective materials, sealing, instrumentation and hazardous-area requirements.
Manage Wet, Corrosive Gas and Package Containment
Biogas can leave a digester saturated with water vapour. If the gas cools in a pipe, filter or blower inlet, condensate may form and carry dissolved contaminants. Upstream separation, drain locations, drain operation and protection against liquid carryover should be designed for the actual temperature profile. A blower should not be expected to handle liquid slugs unless the manufacturer has explicitly approved that condition.
Materials and seals should be reviewed against the worst credible gas and condensate composition, including H₂S, carbon dioxide, oxygen, siloxanes and relevant trace contaminants. Define the acceptable leakage criterion for the complete package, not only the blower casing; include shaft seals, vents, drains, flexible connections, relief and bypass lines, instruments and auxiliary equipment. The containment method and hazardous-area design must match the site risk assessment and applicable project requirements.
Match Capacity Control to the Operating Profile
Biogas flow and downstream demand can vary over a day, season or facility life. A variable-frequency drive can adjust blower speed to follow a pressure, vacuum or flow signal within the machine and motor’s permitted speed range. The control strategy should also respect minimum speed, motor loading, gas temperature, pressure limits and the process’s safe operating range.
Bypass or recycle arrangements may protect equipment or manage short transients, but continuous recirculation can consume power and raise gas temperature. For a broad demand range, staged blower sizes or a base-and-trim arrangement may be more appropriate. Independent pressure or vacuum protection and the plant’s shutdown logic remain necessary even when speed control is installed.
Information Needed for a Project Review
For an initial technical review, provide the following information:
- Process service and flow diagram, including whether the duty is raw-gas transfer, landfill extraction, digester recirculation, upgrading support or process-air supply.
- Minimum, normal and maximum gas composition, including methane, carbon dioxide, H₂S, oxygen/nitrogen, moisture or dew point, and relevant siloxanes, ammonia, VOCs or particulates.
- Required inlet flow with its reference conditions, suction pressure or vacuum, discharge pressure, gas temperature and expected operating duration.
- Upstream separators, filters, treatment equipment, condensate handling, downstream users and the pressure losses or setpoints that govern operation.
- Required control range, start/stop frequency, redundancy, site elevation, ambient conditions, hazardous-area classification and package leakage requirement.
With these inputs, the application can be screened against the machine performance data, gas compatibility and package requirements. Final model selection should follow a duty-point review with the complete process and protection requirements.
Glossary
Air-side process circuit: A dedicated blower and piping path that supplies treatment air and is specified separately from raw-biogas handling.
Gas-duty envelope: The documented range of gas composition, inlet conditions, flow and pressure requirements used to evaluate equipment suitability.
Upgrading-skid interface: The defined connection where a transfer, recycle or auxiliary machine serves a PSA/VPSA package, separately from its principal cycle equipment.
Package-wide containment boundary: The full set of gas-wetted machine and auxiliary components covered by the project leakage criterion.