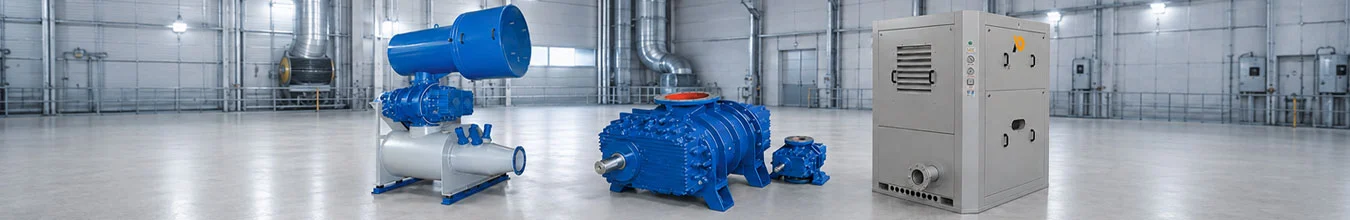
FGD oxidation air supplies oxygen to the absorber slurry, with its duty determined by process load, sparger submergence and system losses. In wet limestone FGD (Flue Gas Desulfurization) systems, sulfur dioxide is absorbed into an alkaline slurry and reacts with calcium-based reagent. Forced oxidation air is then introduced into the slurry to convert calcium sulfite into calcium sulfate dihydrate, commonly known as gypsum.
The oxidation-air system has a direct influence on sulfur-removal stability, gypsum quality, slurry chemistry, scaling behavior and downstream dewatering performance. roots blowers can provide the required oxidation air where the specified airflow and pressure fall within the operating range of positive-displacement rotary-lobe technology.
roots blowers are not the only machines used for this duty. Large FGD installations may employ multistage centrifugal or high-speed turbo blowers, particularly where very high airflow is required. roots blowers are most relevant where the plant requires moderate flow, relatively high differential pressure, stable volumetric delivery, good turndown and mechanically robust operation.
Wet Limestone FGD Process
In a wet limestone FGD absorber, flue gas comes into contact with a recirculating slurry containing finely ground limestone. Sulfur dioxide transfers from the gas phase into the liquid phase and reacts with the alkaline reagent.
A simplified overall reaction is:
Simplified Overall Reaction
This equation combines absorption, neutralization and oxidation into one overall representation. In the actual process, several ionic and intermediate reactions take place.
Without sufficient oxidation, calcium sulfite and bisulfite species remain in the slurry. Forced oxidation converts these compounds into sulfate and encourages gypsum formation.
A simplified oxidation reaction is:
Oxidation Reaction
The theoretical reaction requires half a mole of oxygen for each mole of calcium sulfite. Actual plant air demand is higher because not all oxygen entering the absorber or oxidation tank transfers into the liquid and participates in the reaction.
Function of the Oxidation-Air Blower
The roots blower draws filtered atmospheric air and supplies it to spargers, lances or air-distribution grids submerged in the absorber reaction tank or a separate oxidation vessel. The air passes through openings in the distribution system and forms bubbles in the slurry.
Oxygen transfers from the bubbles into the liquid phase. The dissolved oxygen then supports the oxidation of sulfite to sulfate.
The blower must provide sufficient pressure to overcome:
- Hydrostatic pressure above the sparger
- Sparger or lance pressure loss
- Air-distribution header resistance
- Pipe and fitting losses
- Isolation and control-valve losses
- Inlet-filter resistance
- Fouling of air-distribution openings
- Absorber or tank operating pressure
The roots blower does not determine the chemical oxidation rate independently. Oxidation performance also depends on bubble size, gas distribution, slurry mixing, reaction kinetics, pH, temperature, sulfite concentration, oxygen-transfer efficiency and residence time.
Why Stable Airflow Matters
If oxidation airflow is insufficient, sulfite may accumulate in the slurry. Possible consequences include:
- Reduced gypsum purity
- Poor crystal growth
- Difficult slurry dewatering
- Increased scaling tendency
- Unstable absorber chemistry
- Higher sulfite concentration
- Reduced by-product marketability
- Increased process-control variability
Excessive airflow can also be undesirable. It may cause:
- Unnecessary blower power consumption
- Excessive slurry agitation
- Increased mist formation
- Higher gas load on the absorber
- Accelerated sparger wear
- Higher equipment noise
- Reduced overall process efficiency
The correct objective is not maximum airflow. It is the lowest reliable air supply that maintains the required degree of oxidation and gypsum quality over the complete boiler-load and fuel-sulfur range.
Oxidation-Air Demand
The theoretical oxygen requirement can be calculated from the sulfite oxidation reaction. A simplified design relationship is:
Theoretical Oxidation-Air Demand
- nair,theoretical = theoretical molar airflow
- nO₂,required = stoichiometric oxygen requirement
- yO₂ = oxygen mole fraction in dry air
Because oxygen utilization is not complete, the actual design requirement must account for effective oxygen-transfer efficiency:
Design Oxidation-Air Demand
- nair,design = design molar airflow
- ηO₂ = effective oxygen utilization or transfer fraction
This relationship is useful for understanding the process but should not replace plant-specific mass-transfer testing or FGD process-design data.
Actual oxidation-air demand is affected by:
- Boiler load
- Fuel sulfur content
- Sulfur-dioxide concentration
- Required sulfur-removal efficiency
- Limestone quality
- Absorber slurry pH
- Sulfite concentration
- Slurry solids concentration
- Reaction-tank volume
- Sparger submergence
- Bubble size
- Slurry mixing
- Temperature
- Required gypsum purity
The design should cover the maximum credible sulfur load, not merely normal boiler operation.
Normal and Actual Airflow
FGD process specifications often state airflow in normal cubic metres per hour. The roots blower, however, handles actual inlet volume. These values must not be treated as identical.
For dry air under ideal-gas assumptions, the conversion can be expressed as:
Actual Volume Flow Conversion
- Qactual = actual volume flow at blower inlet conditions
- Qnormal = volume flow at stated normal conditions
- Tactual = absolute blower inlet temperature, K
- Tnormal = absolute normal reference temperature, K
- Pactual = absolute blower inlet pressure
- Pnormal = absolute normal reference pressure
Humidity, inlet-filter pressure loss and site altitude should also be considered when accurate mass-flow determination is required.
At high altitude or elevated ambient temperature, air density decreases. A blower delivering the same actual inlet volume then supplies less oxygen mass. Blower sizing must therefore be based on the lowest expected inlet-air density.
Hydrostatic Pressure
Oxidation air is usually injected below the slurry surface. The blower must overcome the hydrostatic head above the injection point.
The hydrostatic pressure is:
Hydrostatic Pressure (Submergence)
- ΔPliquid = hydrostatic pressure, Pa
- ρslurry = slurry density, kg/m³
- g = gravitational acceleration, approximately 9.81 m/s²
- hsubmergence = vertical depth of the sparger below the slurry surface, m
Slurry density should be used rather than pure-water density. FGD slurry contains suspended limestone, gypsum and other solids, so its density may be substantially higher than that of water.
The maximum credible liquid level and maximum slurry density should be used when determining the blower’s maximum differential-pressure requirement.
Total Blower Differential Pressure
The total pressure requirement can be written as:
Total Differential Pressure
- ΔPliquid = hydrostatic pressure
- ΔPsparger = sparger or air-lance pressure drop
- ΔPpipe = pipeline and fitting losses
- ΔPvalves = isolation and control-valve losses
- ΔPfilter = dirty inlet-filter pressure loss
- ΔPtank = absorber or oxidation-tank internal pressure
- ΔPmargin = justified design allowance
The design margin should account for normal fouling and process variation without hiding an unrealistic or incomplete pressure calculation. Selecting an excessively high blower pressure increases motor power and discharge temperature.
Glossary
Actual air flow: Volume flow evaluated at the blower’s actual inlet conditions.
Calcium sulfite oxidation: Reaction that converts sulfite in scrubber slurry toward sulfate.
Gypsum: Calcium sulfate dihydrate formed in wet limestone FGD systems.
Hydrostatic head: Pressure required to overcome liquid depth above an air outlet.
Oxidation-air demand: Airflow required to supply oxygen for the scrubber reaction.
Sparger pressure drop: Pressure loss through the air-distribution pipe and sparger openings.
Sparger submergence: Vertical depth of the air outlet below the slurry surface.
Stoichiometric oxygen requirement: Theoretical oxygen quantity required for a specified oxidation reaction.