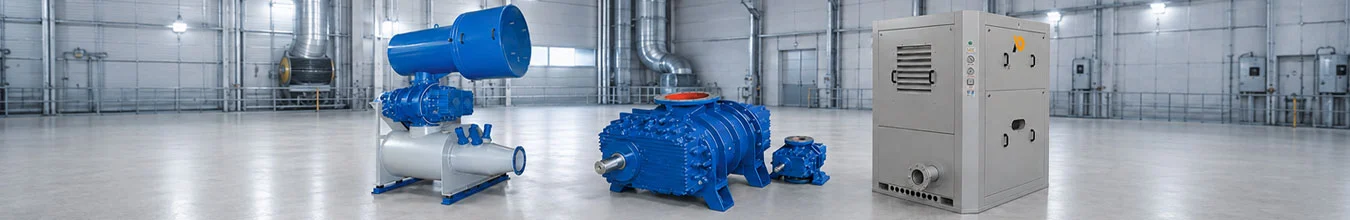
For process-gas duties, roots blowers for the chemical industry must be matched to gas composition, pressure, flow and material compatibility. Fertilizers, polymers, solvents, coatings, detergents, pharmaceuticals, fibres, adhesives, fuels and specialty chemicals are produced through closely connected physical and chemical operations.
Chemical manufacturing is also one of the world’s most economically significant industrial sectors. An international assessment based on 2017 data estimated that the chemical industry supported approximately USD 5.7 trillion in global economic activity and 120 million jobs through its direct, indirect and induced effects. These figures illustrate both the scale of the industry and its extensive connection with other manufacturing sectors.
Many chemical plants operate as integrated production complexes. The product or by-product of one process becomes the feedstock for another, creating interconnected systems for reaction, separation, drying, distillation, gas recovery, solids handling and emissions control. Reliable movement of gases, vapours, powders and granular materials is therefore essential to plant performance.
Roots blowers can perform several of these duties when the required flow and pressure fall within the operating range of positive-displacement rotary-lobe technology.
Process Gas Conveying and Boosting
Chemical and petrochemical plants handle gases with widely different physical and chemical properties. Depending on the process, a roots-type process gas blower may be used to convey, circulate or boost:
- Inert gases
- Hydrocarbon mixtures
- Hydrogen-containing gases
- Synthesis gas
- Carbon dioxide
- Nitrogen
- Solvent vapours
- Vent gases
- Flare-recovery gases
- Off-gases from reactors and separation equipment
- Corrosive or toxic process gases
These applications require specially engineered process gas blowers. A standard roots air blower should not automatically be used for combustible, corrosive or toxic gas service.
The suitability of a blower depends on:
- Gas composition
- Molecular weight
- Inlet pressure
- Required discharge pressure
- Operating temperature
- Condensation behaviour
- Corrosiveness
- Toxicity
- Flammability limits
- Permissible leakage
- Hazardous-area classification
Low-molecular-weight gases such as hydrogen require particular attention because they can produce substantially greater internal and external leakage than air. Gases containing hydrogen sulphide, chlorinated compounds or corrosive vapours may require special casing materials, coatings, shaft seals and purge arrangements.
Oil-Free Gas Path
In a roots blower, the synchronized rotors operate without contacting each other or the casing. Lubricating oil is normally confined to the gear and bearing chambers outside the process space.
When the blower is correctly designed and sealed, the process gas can therefore remain free from lubricating oil contamination. This characteristic is valuable where oil could contaminate a catalyst, react with the conveyed gas, affect product purity or create deposits in downstream equipment.
Oil-free gas handling does not mean that the complete blower contains no lubricant. It means that lubricated mechanical components are isolated from the process chamber. Seal condition and pressure relationships must be controlled to prevent lubricant migration or process-gas leakage.
Flare-Gas and Vent-Gas Recovery
Chemical and petrochemical plants may generate intermittent or continuous gas streams that would otherwise be routed to a flare. Where the gas composition and process economics permit recovery, a gas-tight roots blower may collect and boost the gas for reuse as plant fuel, return to the process or delivery to a treatment system.
The correct term for this application is flare-gas recovery or vent-gas recovery. A flare itself does not require a roots blower simply because it burns process gas.
Recovered gas can contain:
- Condensable hydrocarbons
- Water vapour
- Hydrogen sulphide
- Particulates
- Corrosive components
- Rapidly changing gas compositions
The inlet system may therefore require a knock-out vessel, demister, gas cooler, condensate drainage and liquid-level shutdown. Liquid slugs must not enter the roots blower.
Because flare-header pressure can vary significantly, the blower control system must respond without creating excessive suction that could draw atmospheric air into the gas system. Oxygen ingress may create a flammable mixture and must be prevented by the process design.
Pneumatic Conveying of Chemical Powders
Roots blowers are widely used to supply air or compatible conveying gas for pneumatic transport of powders, granules and other bulk chemical materials.
Typical materials may include:
- Polymer pellets and powders
- Fertilizer products
- Soda ash
- Lime and limestone
- Catalysts
- Activated carbon
- Detergent ingredients
- Pigments
- Resins
- Mineral additives
- Fine inorganic chemicals
- Intermediate products
In a positive-pressure system, the blower is positioned upstream of the material feeding device and supplies clean conveying gas. In a vacuum system, the roots blower operates downstream of the receiver and filtration equipment.
The conveying medium may be atmospheric air, dried air or an inert gas. Nitrogen may be required where the product reacts with oxygen, absorbs moisture or forms a combustible dust atmosphere.
When product purity is important, the blower package should provide an oil-free gas path. The inlet air, silencer construction, filters, piping cleanliness and downstream separator must also satisfy the required contamination limits.
Chemical Fluidized-Bed Processes
Some chemical processes use upward-flowing gas to suspend particles and create fluid-like behaviour within a bed. Fluidized beds can provide intensive gas-solid contact, uniform temperature distribution and effective heat and mass transfer.
Roots blowers may supply fluidization or process air where the required pressure is sufficient to overcome:
- Gas-distributor resistance
- Pressure drop through the material bed
- Piping and valve losses
- Reactor operating pressure
- Filter or separator resistance
The blower must be selected for the maximum expected bed pressure drop, including startup and abnormal bed conditions. Supplying more air than required can increase particle entrainment, filter loading, erosion and energy consumption.
The suitability of a roots blower depends on the reactor pressure. Pressurized fluidized-bed reactors may require higher-pressure compressor technology.
Vacuum Distillation and Solvent Recovery
Vacuum distillation reduces the boiling temperature of a liquid by lowering the pressure above it. This allows heat-sensitive compounds to be separated at temperatures below their atmospheric boiling points.
Roots-type vacuum boosters can increase the pumping speed of vacuum systems used for:
- Vacuum distillation
- Solvent recovery
- Evaporation
- Reactor evacuation
- Process drying
- Degassing
- Vapour extraction
A roots vacuum booster generally operates together with a backing pump. The backing pump establishes and maintains the necessary discharge pressure, while the booster increases gas-handling capacity at lower inlet pressures.
The booster should not be described as a dry-compressing backing pump unless the specific machine has been designed and approved for independent operation over the stated pressure range.
Condensable vapours present a major design challenge. Condensation inside the booster can cause corrosion, deposit formation, rotor contact and overload. The vacuum system may require condensers, knock-out vessels, temperature control, solvent-compatible seals and gas purging.
Glossary
Barrier gas: Clean gas supplied to control migration across a shaft-seal arrangement.
Flare-gas recovery: Capture and transfer of selected gas that would otherwise be sent to a flare.
Gas compatibility: Suitability of wetted materials and seals for the process mixture.
Hazardous-area classification: Designation of locations where flammable gas or dust may create an ignition hazard.
Powder containment: Measures that prevent chemical solids from escaping the transfer system.
Process-gas service: Handling a gas stream defined by composition, flow and pressure conditions.
Seal leakage rate: Quantity of process gas passing through a shaft-seal boundary per unit time.
Vacuum machine class: Equipment specifically designed and rated for a defined vacuum duty.