Vacuum distillation and solvent recovery separate volatile components under reduced absolute pressure, often to limit thermal exposure. Reducing the operating pressure lowers the boiling temperature of the components, making it possible to process heat-sensitive, high-boiling or thermally unstable materials at lower temperatures.
Chemical plants use vacuum distillation for solvent purification, solvent recovery, removal of volatile components, separation of high-boiling products and processing of materials that would degrade, polymerize or react at their atmospheric boiling temperatures.
A roots vacuum booster can significantly increase pumping speed within a defined vacuum range. It normally operates together with a backing pump and should be engineered as part of a complete vacuum system that includes condensers, separators, piping, controls and protective devices.
Why Vacuum Is Used in Distillation
A liquid boils when its vapour pressure becomes equal to the pressure acting on its surface.
For a relatively pure component:
System Pressure
- Psystem = absolute pressure in the distillation equipment
- Psaturation = saturation vapour pressure of the liquid
- Tboiling = boiling temperature at the stated pressure
This provides several process advantages:
- Lower product temperature
- Reduced thermal degradation
- Lower polymerization risk
- Separation of high-boiling compounds
- Reduced heating-medium temperature
- Improved recovery of temperature-sensitive solvents
- Removal of residual volatiles from chemical products
The boiling temperature of a pure component can be estimated using an Antoine-type vapour-pressure equation:
Antoine Equation
- Psaturation = saturation pressure
- T = temperature
- A, B and C = component-specific Antoine coefficients
The pressure and temperature units depend on the coefficient set. Coefficients must not be used with different units or outside their validated temperature range.
Chemical mixtures require vapour-liquid equilibrium calculations. Their boiling behaviour cannot always be represented by the vapour pressure of one pure solvent.
What Is a Roots Vacuum Booster?
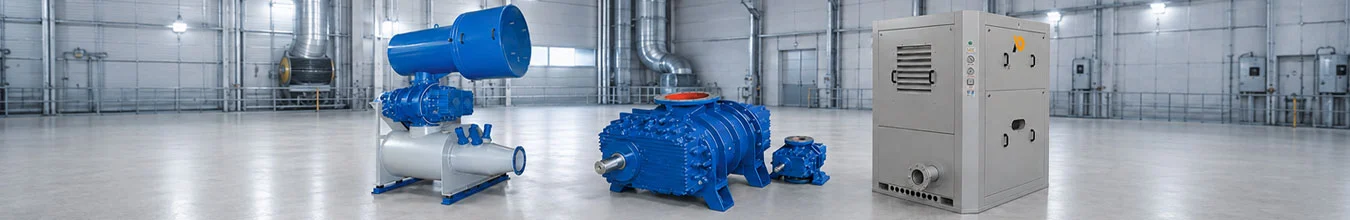
A roots vacuum booster is a positive-displacement machine containing two synchronized lobed rotors. The rotors rotate without contacting each other or the casing, transporting gas from the suction side toward a downstream vacuum pump.
The roots booster is generally installed between the process and the backing pump:
Process vessel → Condenser and separator → Roots vacuum booster → Backing pump → Discharge treatment
The exact arrangement depends on process pressure, vapour load, condensation strategy and equipment compatibility.
The backing pump establishes the initial vacuum and discharges the gas toward atmosphere or another compression stage. The Roots booster increases pumping capacity after the pressure has fallen into its permissible operating range.
It should not normally be described as the backing pump. Most conventional Roots boosters cannot independently evacuate a process from atmospheric pressure because the resulting differential pressure and thermal load would be excessive.
Special booster designs with bypass valves, controlled drives or other overload-protection arrangements may begin operating at higher inlet pressure, but their permissible operating envelope must still be respected.
Benefits of a Roots Booster
A correctly integrated roots vacuum booster can provide:
- High pumping speed at low absolute pressure
- Faster evacuation of process equipment
- Greater vapour-handling capacity
- Improved pressure stability under process load
- Reduced load on the backing pump
- Dry, contact-free gas transport
- No lubricating oil in the booster process chamber
- Adaptability to different backing-pump technologies
- Speed-based capacity control
- Multi-stage vacuum capability
The booster does not create unlimited vacuum. The attainable system pressure depends on gas load, backing-pump performance, piping conductance, condensation, leakage and the pressure ratio across each stage.
Vacuum Distillation Applications
Roots vacuum boosters may be incorporated into systems handling:
- Solvent purification
- Solvent recovery
- Fractional vacuum distillation
- Batch distillation
- Continuous distillation
- Thin-film and wiped-film evaporation
- Removal of residual monomers
- Devolatilization
- Essential and specialty chemical purification
- High-boiling organic compounds
- Heat-sensitive intermediates
- Pharmaceutical intermediates
- Resin and polymer processing
- Used-solvent reclamation
The booster must be selected for the actual vapour composition and expected contaminants. Solvent name alone is not enough to determine suitability.
Solvent-Recovery Systems
Solvent recovery separates valuable or regulated volatile compounds from a process stream so that they can be reused, purified or disposed of in a controlled manner.
A vacuum solvent-recovery system may include:
- Process vessel
- Distillation column
- Reboiler or heated evaporator
- Vapour line
- Partial or total condenser
- Condensate receiver
- Knock-out vessel
- Roots vacuum booster
- Backing pump
- Exhaust condenser
- Scrubber or activated-carbon treatment
- Solvent storage vessel
The condenser should remove as much vapour as practical before the remaining gas reaches the vacuum pumps. Condensing vapour as a liquid is generally more energy-efficient than compressing its entire volume as gas.
The roots booster then handles the non-condensed vapour, permanent gases, air leakage and any purge gas entering the system.
Vacuum-System Gas Load
Vacuum equipment should be selected from the total gas load, not only from the empty-vessel volume.
The total gas load may include:
Total Gas Load
These terms represent:
- Vapour not condensed upstream
- Non-condensable process gas
- Air entering through leaks
- Intentional purge or stripping gas
- Gas released from liquids and solids
- Gas desorbed from internal surfaces
- Gas released during chemical reaction
The dominant load during initial evacuation may differ from the dominant load during steady distillation. Both conditions must be evaluated.
Pumping Speed and Gas Throughput
Vacuum pumping speed is the actual gas volume passing the suction connection per unit time at the stated suction pressure.
Gas throughput can be represented as:
Gas Throughput
- qgas = gas throughput
- Psuction = absolute suction pressure
- S = pumping speed at suction conditions
The approximate pumping speed required at a specified operating pressure is:
Required Pumping Speed
- Srequired = required effective pumping speed
- qtotal = total gas throughput
- Poperating = required absolute process pressure
As the operating pressure decreases, the actual volume associated with a given mass flow increases significantly. This is why vacuum distillation can require high pumping speed even when the gas mass flow appears modest.
Actual Volumetric Flow
A normalized gas flow can be converted to actual vacuum conditions using:
Gas Flow Conversion to Actual Conditions (Normal)
- Qactual = actual volume at vacuum-pump suction conditions
- Qnormal = volume at the stated normal conditions
- Tactual = actual absolute gas temperature
- Tnormal = normal reference temperature
- Pactual = actual absolute suction pressure
- Pnormal = normal reference pressure
- Zactual = compressibility factor at actual conditions
- Znormal = compressibility factor at normal conditions
All pressures must be absolute and all temperatures must be in kelvin.
At a low absolute pressure, the actual volumetric flow can be many times the corresponding normalized flow. Failure to make this conversion can result in a severely undersized vacuum booster.
Glossary
Condenser duty: Heat-removal rate required to condense recovered process vapor.
Condenser temperature: Operating temperature that influences vapor condensation and vacuum-system load.
Gas throughput: Quantity of gas handled, expressed as pressure times pumping speed.
Relative volatility: Measure comparing how readily mixture components vaporize relative to each other.
Solvent recovery: Capture and reuse of solvent removed from a process stream.
Vacuum booster: Pump stage that increases pumping speed within its rated vacuum range.
Vacuum leakage rate: Gas flow entering the vacuum system through leaks and imperfect seals.
Vapor pressure: Pressure exerted by vapor in equilibrium with its liquid at a stated temperature.